


Choosing the Right Industrial Chemical Blending Company for Precision Manufacturing
August 28, 2026
A single batch of off-spec chemicals doesn’t just stall a production line; it can jeopardize months of research and thousands of dollars in downstream materials. You understand that in precision manufacturing, the margin for error is nonexistent. If your current sourcing strategy leaves you questioning batch-to-batch consistency or struggling with the high costs of in-house infrastructure, you’re likely searching for a more stable solution. Partnering with a professional industrial chemical blending company allows you to shift the burden of technical compliance and high-purity sourcing to a dedicated ally who values your success.
We’ll discuss how to evaluate potential partners based on their technical capabilities, scale-up reliability, and adherence to rigorous purity standards. You’ll learn the critical factors to consider when sourcing specific grades, such as ACS or USP, and how a manufacturer-to-user relationship can simplify your supply chain. This guide provides the actionable criteria you need to select a manufacturer that mitigates operational risk and streamlines your path from initial formulation to final delivery.
Key Takeaways
- Learn why treating your industrial chemical blending company as an extension of your quality control team reduces capital expenditure while ensuring formulation expertise.
- Understand how to select the correct ACS Grade, USP Grade, or SEMI Grade to match the purity requirements of your most sensitive manufacturing components.
- Identify critical technical capabilities, such as high-shear mixing, required to manage varying viscosities and complex chemical compositions without compromising stability.
- Discover the streamlined five-step production workflow that moves your product safely from initial consultation and pilot batches to nationwide distribution.
- See how integrated Safety Data Sheet (SDS) management and rigorous compliance standards eliminate variables and lower your overall operational risk.
Evaluating an Industrial Chemical Blending Company for Your Operations
Selecting an industrial chemical blending company is a strategic decision that positions a manufacturer as a functional extension of your own quality control team. When operations scale, the cost of maintaining specialized in-house infrastructure often becomes prohibitive. Outsourcing provides an immediate reduction in capital expenditure while granting access to sophisticated formulation expertise. It’s not just about mixing liquids; it’s about ensuring that every variable, from temperature to agitation speed, is controlled to protect the integrity of your product.
There’s a fundamental difference between basic agitation and industrial-grade blending. If your formulation involves high-viscosity components or requires high-shear mixing to achieve stability, a standard mixing service won’t suffice. Working directly with a manufacturer reduces supply chain friction and ensures that technical requirements are communicated without the distortion of a middleman. This custom manufacturing approach provides the transparency needed for high-stakes industrial applications where precision is non-negotiable.
The Difference Between Toll Blending and Contract Manufacturing
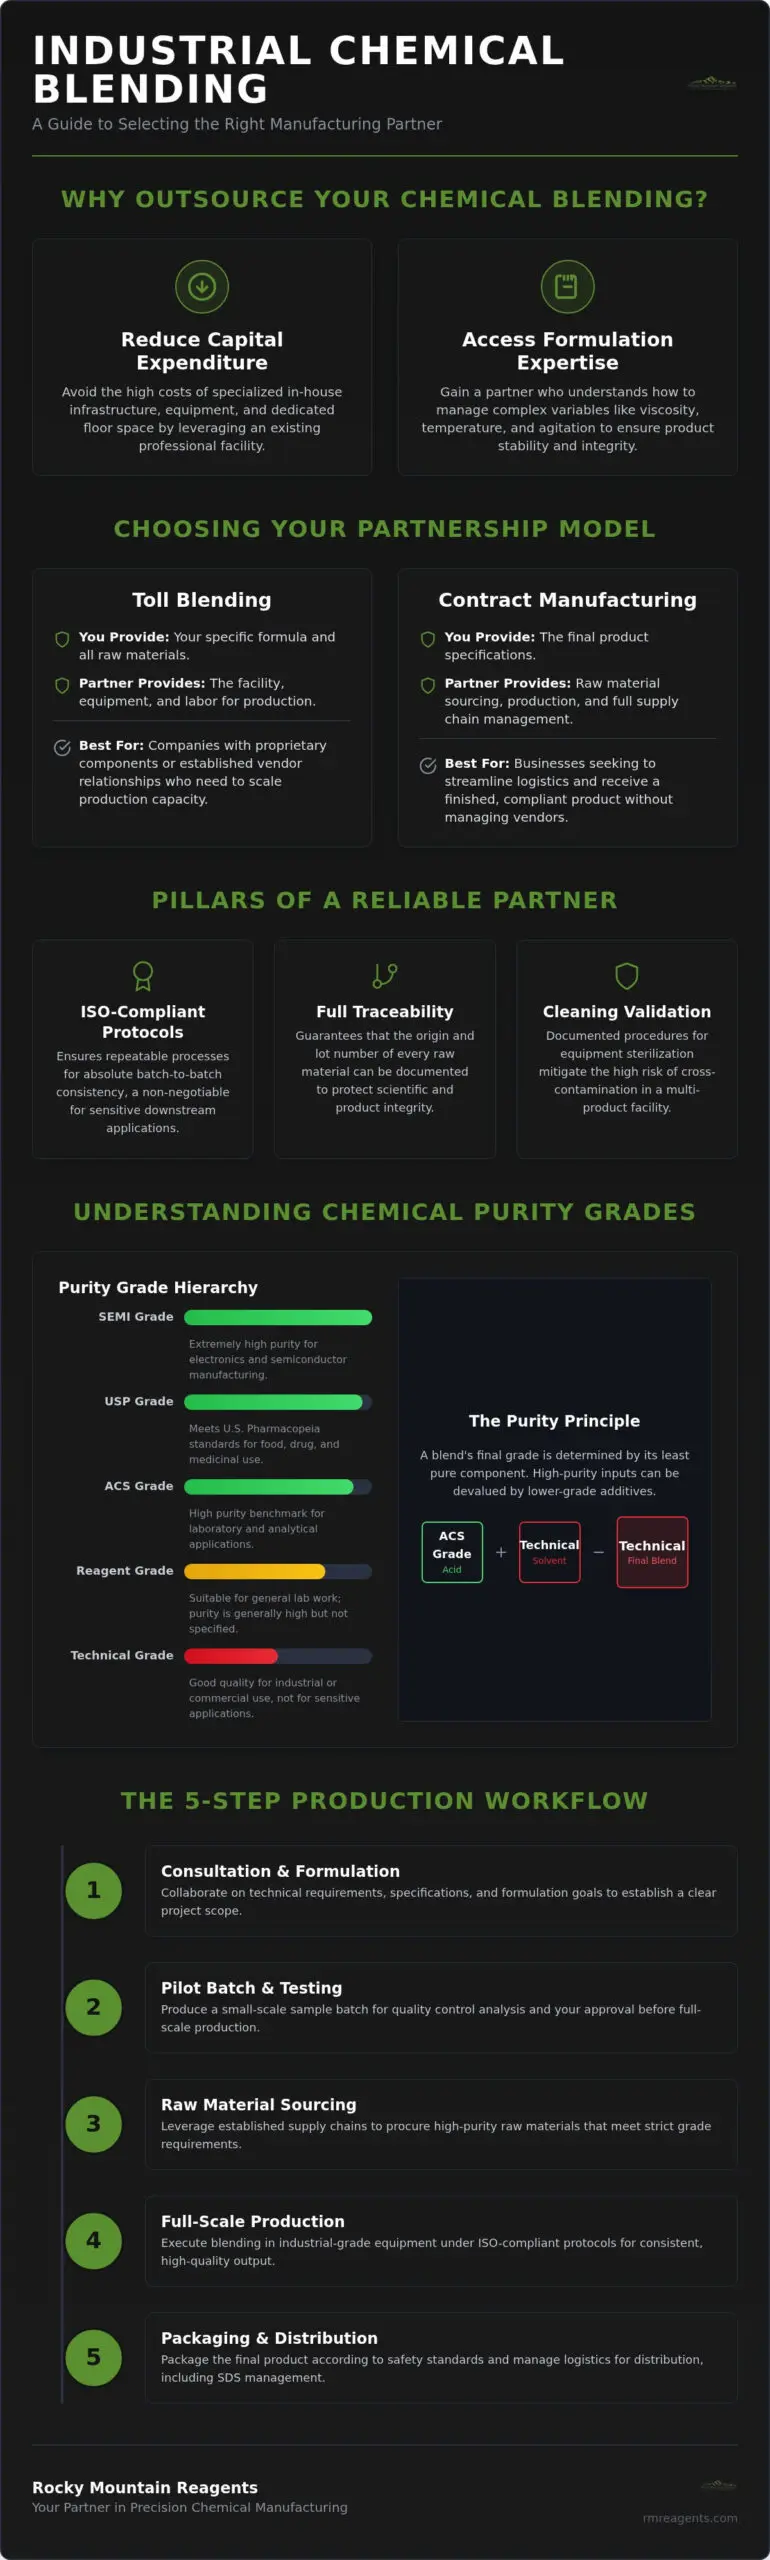
Choosing the right partnership model depends on your existing operational capacity and sourcing preferences. In a toll blending arrangement, you provide the specific formula and the raw materials. The blending partner provides the facility, labor, and equipment. This model works well if you have proprietary components or established vendor relationships you wish to maintain but lack the physical floor space for large-scale production.
Contract manufacturing is a more comprehensive solution where the partner sources all raw materials and manages the entire production cycle. This is often the preferred route for businesses looking to streamline their logistics. If your team is stretched thin, contract manufacturing allows you to receive a finished, compliant product without managing individual material lead times or vendor audits. It shifts the burden of supply chain management to the expert partner.
Key Industry Standards for Blending Facilities
Reliability in chemical production is built on a foundation of rigorous quality standards. ISO-compliant protocols are essential because they dictate the repeatable processes that lead to batch-to-batch consistency. Without these, you risk variations that can ruin sensitive downstream processes. Traceability is another non-negotiable factor. Your industrial chemical blending company must be able to document the origin and lot number of every raw material used in a batch to ensure scientific integrity.
Finally, evaluate the facility’s commitment to cleaning validation. In a multi-product environment, the risk of cross-contamination is high. A professional partner will have documented procedures for equipment sterilization and maintenance to ensure that your ACS Grade or SEMI Grade materials remain uncontaminated by previous production runs. These safeguards protect your brand and your end-users from the risks associated with chemical impurities.
Purity Standards: Navigating ACS, USP, and SEMI Grade Blending
Chemical grades serve as the universal standard for defining the purity levels and application suitability of a substance. In a professional production environment, the final blend must match the grade of its most sensitive component. If you combine an ACS Grade acid with a Technical Grade solvent, the entire batch effectively becomes Technical Grade, regardless of the high-purity component’s cost. Maintaining the integrity of industry monographs, such as those set by the American Chemical Society (ACS) or the Food Chemicals Codex (FCC), ensures that your final product performs predictably in high-stakes environments. When you partner with an industrial chemical blending company, verifying their ability to source and maintain these specific grades is the primary defense against batch failure.
Laboratory Gold Standards: ACS and Reagent Grades
ACS Grade is the benchmark for high-purity laboratory use, meeting the stringent specifications set by the ACS Committee on Analytical Reagents. If a specific ACS standard does not exist for a chemical, Reagent Grade often serves as the next best alternative for analytical work. These grades are non-negotiable when your industrial quality control solutions require absolute precision. Using these standards removes the risk of trace metal contamination that could skew your test results or compromise your manufacturing equipment. It’s a matter of scientific integrity; if the purity is not documented, the results are not reliable.
Specialized Industrial Grades: SEMI, FCC, and USP
Specialized analytical and synthetic applications often require purity levels beyond standard laboratory grades. Absolv™ Grade solvents provide the ultra-high purity required for sensitive synthesis and critical analytical work. In the cannabis industry, High Purity Extraction Grade chemicals are formulated to ensure clean yields without leaving harmful residues. If your work involves liquid chromatography, HPLC and LC-MS Grades offer the specific blending precision needed to prevent column interference. Ensuring your industrial chemical blending company understands these distinctions is the first step in protecting your production line. If you are unsure which grade your application requires, you can consult with our technical team for guidance.
Using Technical Grade chemicals in high-purity applications introduces unpredictable variables. While more cost-effective, Technical Grade is intended for commercial or industrial use where purity is secondary. Introducing it into a precision process can lead to batch failures, equipment corrosion, or safety hazards. Always prioritize the grade that matches your most sensitive requirement to ensure a stable, high-quality outcome.
Core Capabilities: Assessing Technical Blending Requirements
A capable industrial chemical blending company must demonstrate technical proficiency across a wide range of chemical compositions and physical properties. It isn’t enough to simply follow a recipe; the manufacturer needs to understand the physics of the blend. If you’re scaling a specialty product like a disinfectant or sanitizer, high-shear mixing is often essential to create a stable, homogenous emulsion that won’t separate over time. This level of precision requires dedicated onboarding processes where every technical nuance of your formulation is documented and tested before full-scale production begins.
Precision starts with the hardware. Utilizing high-end equipment like OHAUS balances ensures that every component is measured to the exact milligram, eliminating the variance that plagues less disciplined facilities. Whether your project involves delicate titration standards or high-volume industrial cleaners, the goal remains the same: a final product that matches your specification exactly, every single time. This rigorous approach to measurement is what separates a mere supplier from a true manufacturing ally.
Liquid Blending and Viscosity Management
Managing the interaction between acids and bases requires more than just safety protocols; it requires a deep understanding of exothermic reactions and pH stability. Blending acidic, alkaline, or neutral aqueous solutions involves managing heat generation and ensuring the final solution reaches the target concentration without degradation. This is particularly critical when producing heat transfer fluids or buffers that must maintain specific thermal properties or pH levels under operational stress.
Precise viscosity management is equally vital. If a solution is too thick, it may not dispense correctly in your application. If it’s too thin, it may lose its efficacy. For products like indicators and titration standards, even a minor deviation in liquid density can lead to inaccurate laboratory results. A professional partner monitors these variables in real-time, adjusting the process to account for environmental factors like ambient temperature or humidity during the blend.
Custom Formulation and Private Labeling
Transitioning from simple chemical sourcing to custom formulation allows you to develop proprietary products tailored to your specific operational needs. This process often involves individualized chemical synthesis where a partner helps refine your formula for better stability or cost-efficiency. A sophisticated industrial chemical blending company acts as a guardian of your intellectual property, ensuring that your unique formulations are protected through strict internal controls and non-disclosure agreements.
Private labeling services further streamline this process by delivering a shelf-ready product that carries your brand’s identity. This allows you to focus on market growth while your manufacturing partner handles the technical complexities of production, compliance, and quality assurance. It’s a collaborative model that turns a supplier relationship into a strategic manufacturing alliance, providing you with a finished product that meets the highest industry standards without the need for in-house manufacturing overhead.
The Production Workflow: From Formulation to Nationwide Distribution
Transitioning from a laboratory-scale concept to industrial-scale production requires a methodical approach that eliminates variables at every stage. A professional industrial chemical blending company facilitates this through a structured five-step workflow: Consultation, Formulation, Pilot Batch, Production, and Shipping. This sequence ensures that the technical specifications established during initial discussions are faithfully replicated in high-volume batches. Whether you’re scaling a new buffer solution or a complex semiconductor-grade acid, this progression provides a clear roadmap for success.
Safety remains the highest priority during the manufacturing and handling phases. Every technician involved in the process utilizes appropriate personal protective equipment (PPE), including nitrile or latex gloves, to safeguard against chemical exposure. This commitment to safety extends to the end-user through the provision of comprehensive documentation. Accurate Safety Data Sheets (SDS) are non-negotiable; they accompany every blend to ensure your staff has the necessary information for safe handling and regulatory compliance.
Technical Documentation and Regulatory Compliance
Scientific integrity depends on the accuracy of the documentation supporting your chemicals. Every custom formulation must be paired with an up-to-date SDS that reflects the specific hazards and handling requirements of the final blend. If your operations rely on NIST traceable standards for buffer solutions or reagents, your partner must provide the calibration data required for total transparency. You can explore RMR Reagents’ commitment to quality to see how these standards are integrated into daily operations.
Packaging and Logistics for Industrial Chemicals
The final stage of the workflow involves selecting packaging that preserves the purity of the blend while meeting your operational needs. Options range from 100 mL vials for laboratory use to bulk tank loads for heavy industrial applications. Managing the transport of sensitive SEMI Grade materials or corrosive acids requires specialized logistics expertise to prevent contamination or spills during transit. By utilizing a single-source supplier for both chemicals and laboratory equipment, you streamline your procurement process and reduce the risk of supply chain delays.
Nationwide distribution ensures that multi-site industrial operations receive the same consistent product regardless of their location. This uniformity is critical for maintaining quality control across different facilities. When your industrial chemical blending company manages the entire logistics chain, you gain a reliable partner that understands the high-stakes nature of chemical delivery.
Partnering with RMR Reagents for Specialized Chemical Blending
Choosing an industrial chemical blending company is about more than just sourcing a mixture; it’s about securing a defense against the variables that threaten your production. RMR Reagents functions as a sophisticated problem-solver for organizations with complex requirements that generic commodity suppliers can’t meet. Whether your work involves the refined formulations of our Pioneer Forensics brand for blood detection or requires advanced purification and remediation media, we align our internal processes with your technical goals. We assist your team in moving beyond simple procurement toward a relationship built on scientific integrity and shared success.
If your operations require advanced formulations for nutritional testing or specialized buffers, we provide the technical depth necessary to ensure stability. Transitioning from a generic supplier to a dedicated manufacturing partner allows you to focus on your core business while we manage the intricacies of grade selection and compliance. It’s a shift that replaces the risk of the unknown with the assurance of a partner who is deeply invested in the outcome of your scientific work.
Unbounded Excellence in Chemical Manufacturing
Our team leverages decades of technical expertise in handling acids and bases, as well as specialized solvents, to ensure your proprietary formulations remain consistent. We provide a national service footprint that eliminates the logistical limitations of local-only suppliers without the heavy overhead that drives up costs. This streamlined, manufacturer-to-user relationship removes the middleman, allowing for faster response times and more accurate technical alignment. You can request a custom chemical solution to begin the process of optimizing your specialized production line.
Support for High-Precision Research and Industry
High-precision industries like electronics and cannabinoid production require materials that exceed standard expectations. We provide SEMI Grade acids for semiconductor manufacturing and high-purity extraction materials designed for clean, reliable yields in the 710 sector. Our technical support team acts as a dedicated ally to engineers and quality professionals, helping them solve sourcing challenges for hard-to-find components or specialized reagents. We don’t just deliver chemicals; we provide the expertise needed to navigate complex regulatory and technical landscapes.
Through our strategic partnerships with industry leaders like Across International and Adam Equipment, we also ensure you have access to the high-end equipment necessary for accurate measurement and processing. This holistic approach combines high-purity chemistry with precision hardware, creating a unified solution for your facility. If your current supply chain is plagued by batch-to-batch inconsistency, transitioning to an industrial chemical blending company like RMR Reagents is the most effective way to secure your operational future.
Securing Your Production Future Through Precision Blending
Achieving consistent batch quality requires a transition from simple procurement to a dedicated manufacturing alliance. By prioritizing rigorous ACS Grade and USP Grade compliance, you eliminate the variables that lead to costly downtime or regulatory friction. Whether your operations demand specialized SEMI Grade materials for electronics or complex custom formulations, a professional industrial chemical blending company provides the technical depth needed to scale with confidence.
Streamlining your production from initial formulation to nationwide industrial chemical distribution ensures that every facility receives the same high-purity product. This methodical approach protects your brand’s integrity and allows your team to focus on innovation rather than supply chain instability. Relying on a partner that understands the high-stakes nature of scientific precision is the most effective way to mitigate operational risk and ensure long-term stability.
Our team is ready to assist you in optimizing your formulations and ensuring your production lines remain efficient, compliant, and productive. We look forward to helping you achieve a new standard of excellence in your manufacturing operations.
Frequently Asked Questions
What is the difference between toll blending and contract blending?
Toll blending involves a relationship where you provide the formulation and raw materials while the manufacturer provides the labor and equipment. Contract blending is a more comprehensive service where the industrial chemical blending company sources all raw materials and manages the complete production cycle. Deciding between them depends on your internal procurement capacity. If you have proprietary materials, tolling is often preferred; otherwise, contract manufacturing simplifies your logistics by utilizing a single-source partner.
How do I choose the correct chemical grade for my industrial application?
You should select a chemical grade based on the highest purity requirement of your specific application. ACS Grade is the standard for analytical work, while USP Grade meets the requirements for pharmaceutical research and educational settings. For electronics manufacturing, SEMI Grade is necessary to prevent metallic contamination. Using the wrong grade can lead to batch failure or equipment damage. Always verify the industry monograph requirements before finalizing your blending specification to ensure compliance and stability.
What technical documentation should I expect from a blending company?
A professional partner must provide a comprehensive Safety Data Sheet (SDS) for every custom blend to ensure safe handling and regulatory compliance. You should also receive a Certificate of Analysis (CoA) that documents the specific purity levels and batch lot numbers. If your work involves buffer solutions, expect NIST traceable documentation to verify calibration accuracy. These documents are essential for maintaining scientific integrity and providing a clear audit trail for your quality control team.
Can an industrial blending company help with custom chemical formulations?
Yes, a sophisticated industrial chemical blending company can assist with the development and refinement of proprietary formulations. This process typically starts with a technical consultation to analyze your specific requirements and performance goals. The manufacturer then produces pilot batches to test stability and efficacy before scaling to full production. This collaborative approach allows you to leverage expert chemical synthesis without the need for an expensive in-house laboratory infrastructure or specialized engineering staff.
What are the risks of using technical grade chemicals in scientific research?
Technical Grade chemicals contain unpredictable levels of impurities that can skew analytical results or contaminate sensitive equipment. These grades are intended for commercial use where high purity isn’t a priority. In scientific research, trace contaminants might cause unintended side reactions or interfere with liquid chromatography. Choosing a higher grade, such as ACS Grade, removes these variables and ensures that your results are repeatable and your laboratory environment remains free from unnecessary chemical interference.
How does an industrial blending company ensure batch-to-batch consistency?
Consistency is achieved through rigorous adherence to ISO-compliant protocols and the use of precision equipment like OHAUS balances. A manufacturer must implement strict cleaning validation procedures to prevent cross-contamination between different production runs. Every variable, including mixing speed, temperature, and order of addition, is documented in a master batch record. These controls ensure that the final product remains identical across every delivery, protecting your downstream processes from the risks associated with batch variation.
Does RMR Reagents provide nationwide shipping for bulk chemical blends?
RMR Reagents provides nationwide service across the United States for all custom blending projects. We manage the logistics for various volumes, ranging from 100 mL vials to bulk tank loads. Our team is experienced in handling the transport of sensitive SEMI Grade materials and corrosive acids, ensuring they arrive safely at your facility. This national footprint allows multi-site industrial operations to maintain a single-source supplier relationship, which simplifies procurement and ensures product uniformity across all locations.
What safety protocols are required for handling concentrated acids during blending?
Handling concentrated acids requires strict adherence to safety protocols, including the use of specialized personal protective equipment like nitrile or latex gloves and face shields. Technicians must work in environments with proper ventilation or fume hoods to manage hazardous vapors. Every process follows the specific instructions found in the applicable Safety Data Sheet (SDS). It’s also critical to use secondary containment and have appropriate spill neutralization materials readily available to mitigate risk during the blending and packaging stages.
Disclaimer
The information provided in this article is for general educational and informational purposes only and is not intended to replace product-specific technical documentation, Safety Data Sheets (SDS), professional advice, or applicable regulatory requirements. Chemical properties, applications, handling procedures, and regulatory requirements may vary by product, concentration, use, and jurisdiction. Always review the applicable SDS and product documentation and follow appropriate workplace safety procedures before handling or using any chemical product. Contact Rocky Mountain Reagents for product-specific specifications or technical information.

